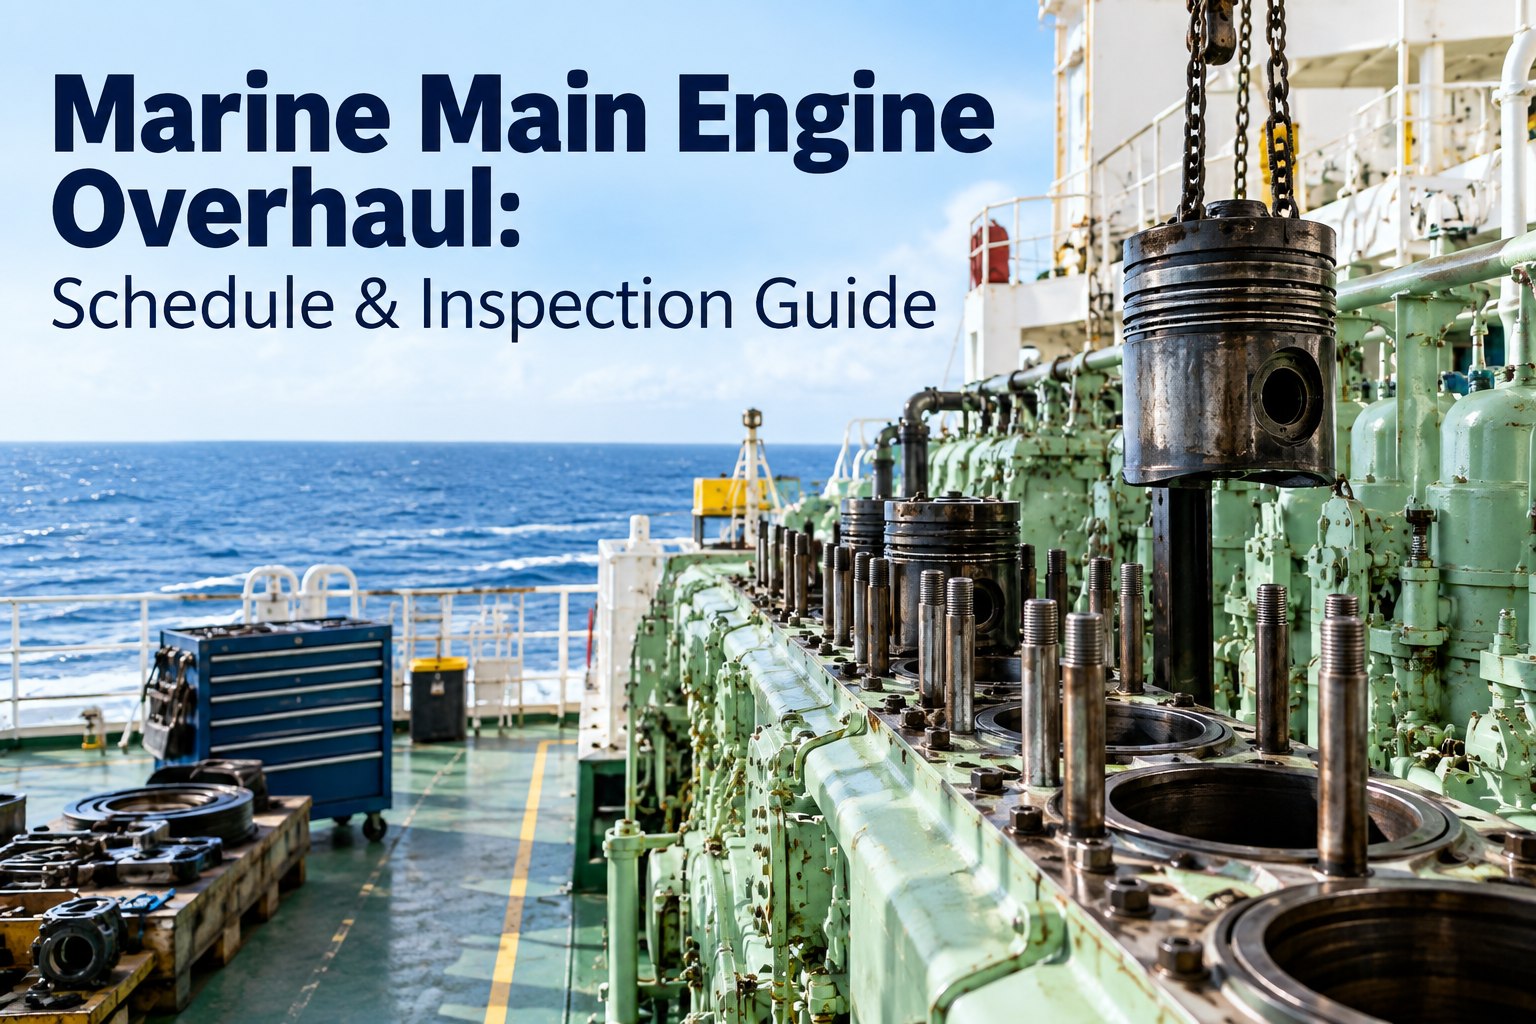
Main engine overhauls are the largest planned maintenance events on most ships, and the ones where getting the timing wrong costs most. Overhaul too early and you spend crew time, spares and off-hire on components that still had thousands of hours left. Overhaul too late and liner wear, ring blow-by or a bearing running hot turn a planned job into a breakdown, a scavenge fire or a class condition. The engine builder's manual is always the authority on intervals, limits and procedures for your specific engine. What this guide adds is the planning layer around it: how running-hour intervals fit together, what to measure and record at each opening, the wear and clearance limits commonly used to judge whether a component goes back in, and how to line the work up with class survey requirements so the evidence counts. If you record this work on paper or in spreadsheets, try Marine Inspection free and keep running hours, measurements and photos with the job.
Three clocks run at once on a main engine: running hours since the last opening, measured condition, and the class survey cycle. This guide brings them together.
The intervals that structure the plan
Intervals vary widely between engine types, fuels and makers, and modern two-stroke designs run far longer between openings than older ones. Use the ranges below only to shape the plan, then set the actual figures from your own manual and your recorded wear rates.
Illustrative spacing. Condition-based overhaul stretches these intervals where wear rates, performance data and scavenge inspections support it. One well-documented case extended a small-bore two-stroke to its first major overhaul at just over 22,000 running hours.
Cylinder liner: the measurement that drives the decision
Liner calibration turns opinion into a number. Gauge at fixed positions down the swept length, in both fore-aft and port-starboard directions, using the maker's template so readings repeat between overhauls. Wear is greatest near top dead centre, and the port-starboard axis usually wears faster because of connecting rod angularity, which is what produces ovality.
What to inspect, measure and decide at each opening
Every component pulled should leave the engine room with three things recorded: a measurement, a comparison with the last one, and a decision. Photographs at the same angles each time make the comparison far easier, especially for ring condition and crown burn-off.
- Crown burn-off and topland wear against the maker's limits
- Ring free gap, butt clearance and groove wear
- Ring movement, breakage or collapse, and blow-by marks
- Cooling bore or crown cooling space condition
- Calibration at all template positions, both axes
- Ovality and wear rate since last reading
- Scuffing, micro-seizure, corrosive wear and cracks
- Honing to restore the running surface where appropriate
- Rod surface condition and scoring
- Scraper ring wear and spring condition
- Drain quantity and appearance, an early sign of trouble
- Clearances by bridge gauge or feeler, against the manual
- Crankshaft deflections, compared with the last set
- White metal condition, wiping, cracks and oil holes
- Bolt tightening records and hydraulic pressures used
- Injector opening pressure and spray pattern
- Valve seat condition, rotator and spindle wear
- Hydraulic and air spring leakage checks
- Deposits, oil accumulation and drain condition
- Ring condition seen through the ports
- Turbocharger fouling, vibration and bearing hours
Line the work up with class survey requirements
Overhaul work only counts as survey evidence if it is examined and recorded the way class expects. Most fleets use a continuous survey arrangement, where machinery items are opened and examined in rotation across the five-year cycle, or an approved planned maintenance scheme based on the maker's intervals and the ship's records. Either way, the records are the deliverable. Our guide to a class-aligned planned maintenance system covers the approval side.
Symptoms that should move an overhaul forward
Condition-based planning only works if deviations are acted on. Treat these as triggers to inspect early rather than waiting for the hour count.
Planning the overhaul itself
The mechanical work is only part of it. Most delays come from spares, manpower and permits rather than the engine. Build the plan around these six items, and keep the whole package in one record so the next crew inherits it.
Frequently asked questions
On the maker's running-hour interval, adjusted by condition. Modern two-stroke engines commonly run many thousands of hours between piston overhauls, and documented cases exist of first major overhauls beyond 20,000 hours where condition supported it.
Generally when wear reaches about 0.6% to 0.8% of the original bore, or the maker's limit, or earlier if scuffing, cracks or a rising wear rate make it unsafe to continue.
Published guidance for two-stroke engines generally falls in the range of roughly 0.05 to 0.1 mm per 1,000 running hours. Compare your own trend against your engine's history rather than a single figure.
Under some class arrangements, certain machinery items can be examined by a qualified chief engineer and confirmed by the surveyor, subject to the society's conditions. Confirm the scope with your class society before the job.
Measurements, clearances, parts fitted, running hours and sign-off, kept for the class cycle and available to surveyors and PSC. See our guide to weak maintenance records.
Marine Inspection records running hours, measurements, clearances and photos at the machine, offline, then builds the wear trend and the survey pack from the same data.