Dredging is the only marine sector paid by the cubic metre rather than by the day, and that single fact should reorganise how a dredging contractor thinks about maintenance software. Production for a hydraulic dredge is the quantity of solids transported — the average slurry flow rate multiplied by the average percentage of solids — and a production estimate determines how long a project takes, which determines what it finally costs. As the standard engineering guidance puts it, the longer a job takes the higher the final cost. Every component that wears reduces one of those two variables. A degraded impeller cuts flow. Worn cutter teeth reduce cutting efficiency and therefore the solids concentration reaching the pump. Neither shows up as a breakdown until much later, but both show up in the production figure immediately. Meanwhile the wear parts themselves are not maintained in any conventional sense: high-chrome cutter teeth and impellers running at chromium contents in the region of 26 to 30 percent are typically quoted with wear lives of six to twelve months, because they are consumed by the work rather than serviced through it. That is a different maintenance model, and it needs a different system. Start a free trial of Marine Inspection and build it around production rather than around the calendar.
The Equation That Governs Everything Else
Average slurry flow rate
multiplied by
Average percent solids
equals
Production
Flow rate falls when
Impeller wear, liner wear, suction or discharge pipeline restriction, cavitation, or reduced available power. Every one of these is a maintenance condition rather than a site condition.
Percent solids falls when
Cutter teeth and adaptors wear, cutter drive power degrades, or the cutter cannot break the face efficiently. Again, maintenance rather than geology, though geology sets the rate of wear.
Which means
Production rate is a condition monitoring signal. A dredge losing ten percent of production over three weeks is telling you something about its wear parts long before anything fails, provided somebody is holding the production data and the maintenance record in the same place.
Paid by the Cubic Metre, Not by the Day
This is the commercial structure that makes dredging maintenance unlike every other sector in this series, and it changes what a maintenance system has to report. Book a Marine Inspection demo and see maintenance cost allocated to a project rather than to a calendar year.
How the money works
A project has a fixed quantity to move. The contractor estimates production, derives a duration from it, and prices the work accordingly. If actual production falls below estimate, the duration extends and the margin erodes against a price already agreed and signed.
Nobody pays more because your pump wore out. Industry cost analysis in this sector is conducted per cubic yard or per cubic metre for exactly that reason — the unit of account is volume, and time is only relevant as the thing that consumes cost while volume is being moved.
That inverts the usual relationship between maintenance and commercial performance. On most vessels, maintenance protects an asset that earns by the day. On a dredge, maintenance protects the production rate itself, which means a worn component is not a future breakdown risk but a present reduction in revenue per hour worked.
The variables you do not control
Actual production varies with soil type, site conditions and dredge master experience, and can differ substantially from nameplate capacity. A unit rated at a given flow may deliver a fraction of it in the material actually encountered. These are estimating risks rather than maintenance failures.
The variables you do control
Wear part condition, pump and cutter drive availability, spares on site, and downtime. These are the ones a maintenance system exists to manage, and they are also the ones most often conflated with the first group when a project underperforms and nobody can separate the causes.
Why separating them matters
Without a record that ties production, wear and downtime together per project, every underperforming job is attributed to difficult ground. Sometimes that is true. Sometimes the teeth were past their useful life for the last third of the job and nobody had the data to say so, which means the same mistake is priced into the next tender.
Wear Parts Are Consumed, Not Maintained
A conventional planned maintenance system schedules overhauls against running hours. Dredging needs something structurally different, because the primary components are consumables with a working life measured in months and a replacement decision driven by production rather than by an interval. Sign up for Marine Inspection and track wear parts as stock, cost and condition rather than as maintenance tasks.
Cutter teeth and adaptors
Teeth are mounted to the cutter head through adaptors, which makes both the tooth and its adaptor wear items on separate replacement cycles. High-strength alloy teeth, typically quoted at chromium contents around 28 to 30 percent, are specified to break compacted silt, gravel and soft rock reaching compressive strengths in the region of 50 megapascals.
Track: position on the head, hours since fitted, material dredged, replacement reason
Pump impellers
High-chrome impellers in the region of 26 to 28 percent chromium, with blade counts chosen for the duty — three-blade and four-blade designs optimise differently for head against flow, which matters when slurry has to travel long distances through floating or onshore pipeline.
Track: hours, production while fitted, flow degradation over life, replacement threshold
Pump liners and casings
Wearing continuously alongside the impeller and frequently replaced on a different cycle. Manufacturer performance figures commonly quote wear lives in the six to twelve month range for components in this duty, though actual life is governed by the material being pumped rather than by elapsed time.
Track: thickness measurements where taken, hours, and correlation with material type
Suction and discharge pipeline
Floating and onshore pipeline carrying abrasive slurry over distances that can extend to several kilometres. Wear is uneven, concentrated at bends and transitions, and pipeline rotation to even it out is a maintenance practice that only works if somebody records which section went where.
Track: section identity, position in the line, rotation history, wall thickness
Spud poles and ladder
The spud poles anchor the dredger and absorb the strong reaction forces generated during cutting, transferring them into the ground. The ladder forms the connection between cutter head and vessel. Both are structural rather than consumable, and both accumulate fatigue in a way that is easy to ignore until it is not.
Track: inspection findings, weld condition, cumulative dredge hours
Why this needs a different system shape
A conventional CMMS asks when a job is next due. A dredging operation needs to know how much life is left in a set of teeth, what production has done since they were fitted, what is on site as spare, what the replacement will cost, and which project the cost belongs to. Those are inventory, production and cost questions wearing a maintenance hat.
The wear register is the core record, not a sub-module of it
6 to 12 months
Typical Wear Life Means Replacement Is the Maintenance Model
Wear parts held individually with fitted date, dredge hours since fitting, material dredged, production while in service and replacement cost — alongside spares on site, lead times and the project the cost belongs to. Captured on the dredge by the crew who change them, offline, in the conditions the work actually happens in.
Three Counters, Not One
Most maintenance systems carry a single running-hour counter per asset. A dredge needs at least three, because different components wear against different clocks and confusing them produces intervals that are either wasteful or dangerous. Schedule a walkthrough and see triggers running against the correct counter for each component.
Counter 1
Engine and generator hours
Elapsed running time on prime movers, generators and auxiliaries. This is the conventional counter and it governs conventional machinery maintenance — oil changes, filter intervals, overhauls. It accumulates whether or not the dredge is producing.
Drives: machinery maintenance intervals
Counter 2
Dredge hours
Time spent actually cutting and pumping, which is materially less than elapsed time once repositioning, waiting, pipeline moves and weather are removed. Production planning works on effective dredging hours per day precisely because the difference is large.
Drives: cutter, pump and wear part life
Counter 3
Cubic metres moved
The commercial counter, and arguably the truest wear measure, because a wear part's life is consumed by material passing through it rather than by time passing. Two identical impellers on identical dredge hours in different material will not have identical remaining life.
Drives: cost allocation and the real wear rate
And one modifier
Material type
Fine sand, silt, clay, coarse sand, gravel and soft rock consume wear parts at wildly different rates. A wear register that records what was being dredged while a component was fitted turns replacement history into a forecasting tool for the next project in similar ground.
Drives: the ability to estimate rather than guess
The Wear and Asset Register
Below is what a dredging operation actually needs to hold, and where each item usually goes missing. Start a free trial and load one dredge's wear register during the evaluation.
Table 1: What the Register Has to Carry
A tooth changed on deck at 0300 should be recorded in seconds, by the person who changed it, with the hours and the material attached.
Three Fleet Types, Three Maintenance Shapes
A mixed dredging fleet is not one maintenance problem repeated. The three principal types wear differently, are positioned differently and fail differently. Book a walkthrough and see each type configured to its own wear profile rather than to a single template.
Cutter suction
Stationary, spud-anchored, pipeline discharge
Anchored to the ground by spud poles which absorb and transfer the strong reaction forces generated while cutting. The cutter head is mounted through a ladder forming a largely rigid connection to the vessel, and the head is lowered on a slant until it reaches the bottom or maximum depth. Movement around the spud is worked by slacking and heaving anchor wires.
Wear concentration: cutter teeth, adaptors, pump, pipeline. The highest consumable burden of the three.
Trailing suction hopper
Self-propelled, cyclical, hopper discharge
Works underway, filling a hopper and discharging by dumping, pumping ashore or rainbowing. Large units in this class operate at the top of the capacity and depth range and carry correspondingly large capital values, which changes the economics of downtime substantially.
Wear concentration: draghead, suction tube, pumps, hopper and discharge system. Cyclical loading rather than continuous.
Backhoe and mechanical
Pontoon-mounted, spud-positioned, bucket excavation
Mechanical dredging lifts sediment out of the water using buckets rather than pumping it as slurry, which removes the pump wear problem entirely and replaces it with a hydraulic and structural one. Production is governed by cycle time rather than by flow and solids concentration.
Wear concentration: bucket teeth, hydraulics, boom structure, spuds. No slurry path to maintain.
Cost Has to Land on a Project
The final structural requirement, and the one most conventional maintenance software fails outright. Start a free trial and see maintenance cost allocated by project rather than by financial year.
The wrong report
Maintenance cost per vessel per year. Useful to a finance department closing a set of accounts, and close to useless to an estimator pricing the next job.
It cannot answer the only question that matters at tender stage: what did it cost us in wear parts and downtime to move a cubic metre of this particular material with this particular dredge. Without that figure, consumable cost is estimated from memory, from the last invoice, or from a supplier's quoted wear life.
The same limitation applies to underperformance. When a project runs long, a vessel-and-year cost report cannot separate difficult ground from degraded equipment, so the explanation defaults to ground conditions and the same assumption is priced into the following tender.
What ownership cost actually comprises
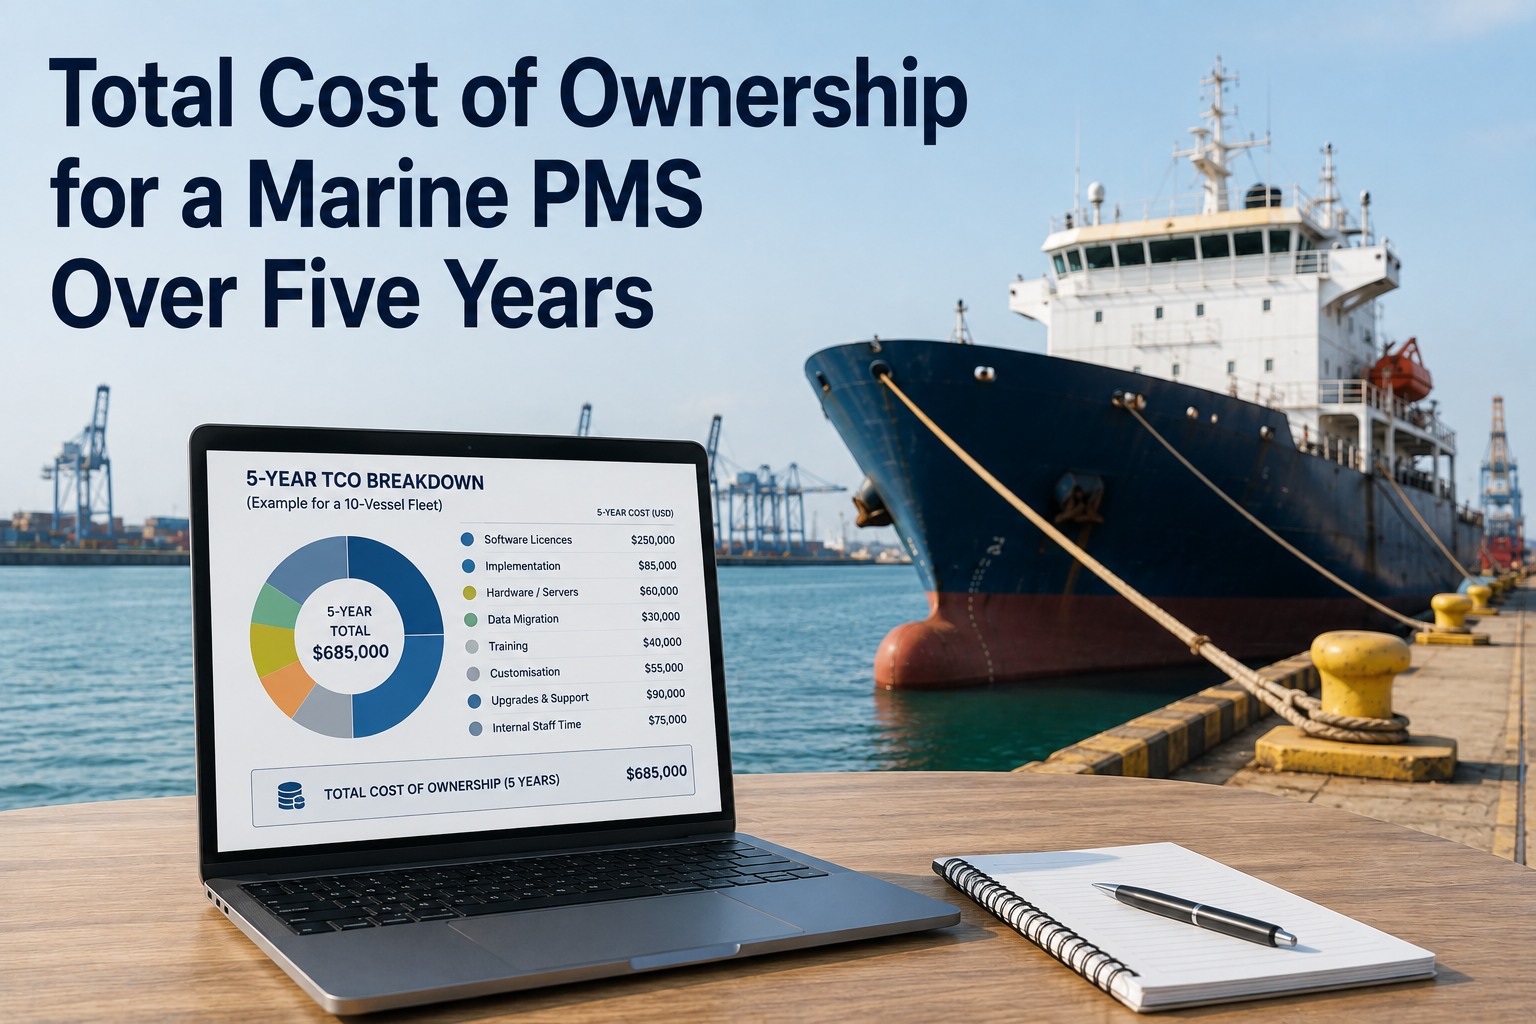
Industry analysis of total ownership cost puts initial purchase at roughly sixty to seventy percent, with operating expenses covering fuel and power, maintenance and labour, and downtime making up the remainder. Maintenance and downtime are the components a contractor can influence after the purchase decision is made.
The report worth building
Wear part cost per cubic metre, by dredge and by material type, across completed projects. That is a tendering asset. It converts a maintenance record into pricing intelligence, and it is only possible if consumption, production and material type were captured together at the time.
The downtime line
Downtime on a dredging project is not a maintenance metric, it is a schedule metric, because a day lost extends the project and the longer a job takes the higher the final cost. Recording the cause of every stoppage against the project is how a contractor learns whether the last overrun was ground conditions or availability.
Evaluating a Platform for a Dredging Fleet
Generic marine maintenance software is built around scheduled overhauls on a single running-hour counter. These questions expose whether a platform can handle a consumable-led, production-driven operation. Schedule a demo with a dredge master and a plant manager present.
Table 2: Buyer Questions Specific to Dredging Operators
2026 DREDGING OPERATIONS REALITY
Capacity and cost figures in this sector are vendor-published. Flow rates, wear lives, efficiency percentages and price ranges circulating in the market come from manufacturers and equipment brokers rather than from independent testing, and they vary widely by source. Treat quoted wear lives and nameplate capacities as starting points for your own measurement rather than as specifications. Actual production is site-specific. Published guidance is explicit that real production varies with soil type, site and operating conditions and dredge master experience, and can sit well below nameplate capacity. Your own historical data on comparable material is worth more than any manufacturer figure. Classification applies to dredging units. Societies issue dredging unit notations and survey these vessels like any other, so class survey windows, certificates and statutory obligations run alongside everything described here. Where ISM applies it applies fully. Element 10's documented maintenance system requirement does not soften because the vessel is a plant item that happens to float.
Frequently Asked Questions
Why does dredging need different maintenance software from other vessels?
Because the primary maintenance objects are consumables rather than serviceable machinery, and because the vessel is paid by volume rather than by time. Cutter teeth, adaptors, impellers and pump liners are consumed by the material passing through them, with manufacturer-quoted wear lives commonly in the six to twelve month range, so the operative questions are how much life remains, what is on site as spare, and what the replacement will cost. Meanwhile production — average slurry flow rate multiplied by average percent solids — determines project duration and therefore final cost, which makes wear condition a commercial variable rather than only a technical one.
What is the difference between dredge hours and engine hours?
Engine hours accumulate whenever a prime mover runs, including repositioning, waiting, pipeline moves and standby. Dredge hours count only time spent actually cutting and pumping, and the gap between the two is substantial — production planning works on effective dredging hours per day precisely because elapsed time overstates productive time considerably. Machinery maintenance intervals should run against engine hours because that is what wears the engine. Cutter, pump and wear part life should run against dredge hours, or better still against cubic metres moved, because that is what consumes them.
Why record what material was being dredged?
Because it is the single biggest determinant of wear rate, and without it replacement history cannot be interpreted. Fine sand, silt, clay, coarse sand, gravel and soft rock consume high-chrome components at very different rates, and cutter teeth are specified to break material with compressive strengths reaching around fifty megapascals. Two identical impellers with identical dredge hours in different ground will have very different remaining life. Recording material type against a component's service period converts a replacement log into a forecasting tool, which lets you estimate consumable cost for the next project in comparable ground rather than guessing.
How does production data help maintenance?
It works as condition monitoring without any additional instrumentation. Production is flow rate multiplied by percent solids, and both variables degrade as components wear — impeller and liner wear reduce flow, while worn cutter teeth and adaptors reduce cutting efficiency and therefore the solids concentration reaching the pump. A dredge losing production steadily over several weeks in consistent material is reporting wear before anything fails. That signal is only available if production figures and the wear register sit in the same system, which is why separating them into a production spreadsheet and a maintenance database loses most of the value of both.
How should maintenance cost be reported for a dredging contractor?
Per project and per cubic metre, not per vessel per year. Industry analysis of total ownership cost puts initial purchase at roughly sixty to seventy percent, with operating expenses and downtime accounting for the rest — and maintenance and downtime are the parts a contractor can influence after purchase. Wear part cost per cubic metre, broken down by dredge and by material type across completed projects, is a tendering asset rather than an accounting output. It is also only constructable if consumption, production, material type and downtime cause were all captured against the project at the time rather than reconstructed afterwards.
Do cutter, hopper and backhoe dredgers need different configurations?
Yes, because they wear in fundamentally different places. A cutter suction dredger is spud-anchored with reaction forces transferred through the spuds, carries a cutter head on a ladder, and concentrates wear in teeth, adaptors, pump and pipeline — the heaviest consumable burden of the three. A trailing suction hopper dredger works underway on a cyclical fill-and-discharge pattern, with wear in the draghead, suction tube, pumps and discharge system. A backhoe lifts material mechanically rather than pumping slurry, which removes the pump wear problem entirely and replaces it with hydraulic and structural maintenance governed by cycle time. One template across all three will fit none of them well.
Cutter, hopper and backhoe fleets
Maintenance Measured in Cubic Metres
Because that is how you get paid
Wear parts held individually by fitted position with dredge hours, material type and production while in service. Separate counters for engine hours, dredge hours and volume moved. Spares by project site with consumption rates and lead times. Downtime cause captured at the stoppage. And consumable cost per cubic metre by dredge and by material, ready for the next tender — recorded on deck in seconds, offline, by whoever made the change.